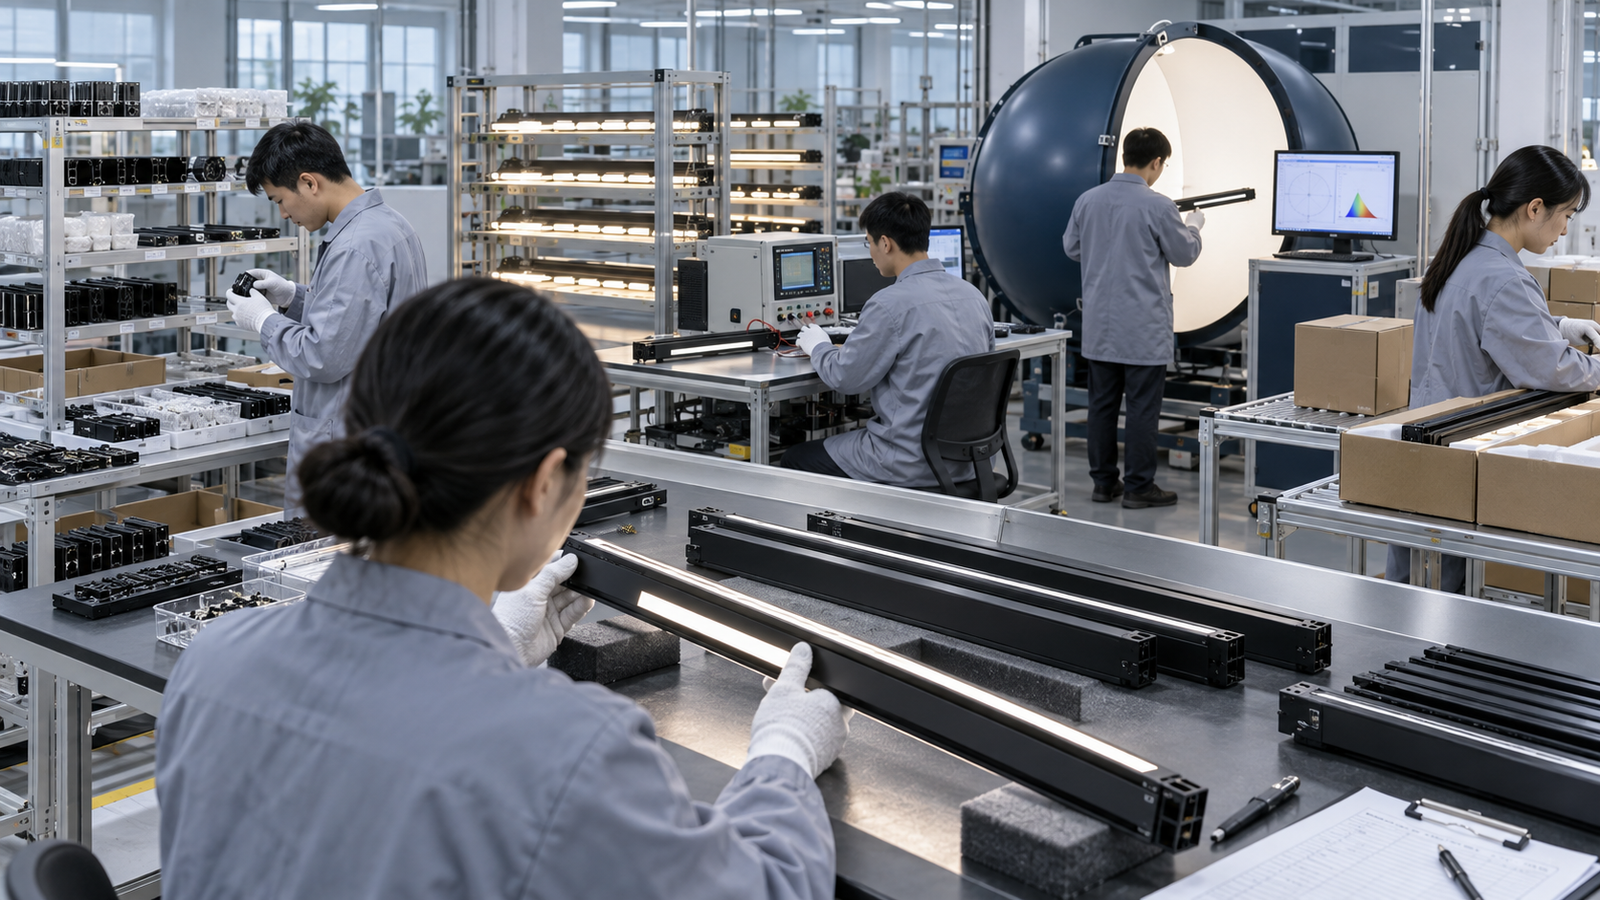
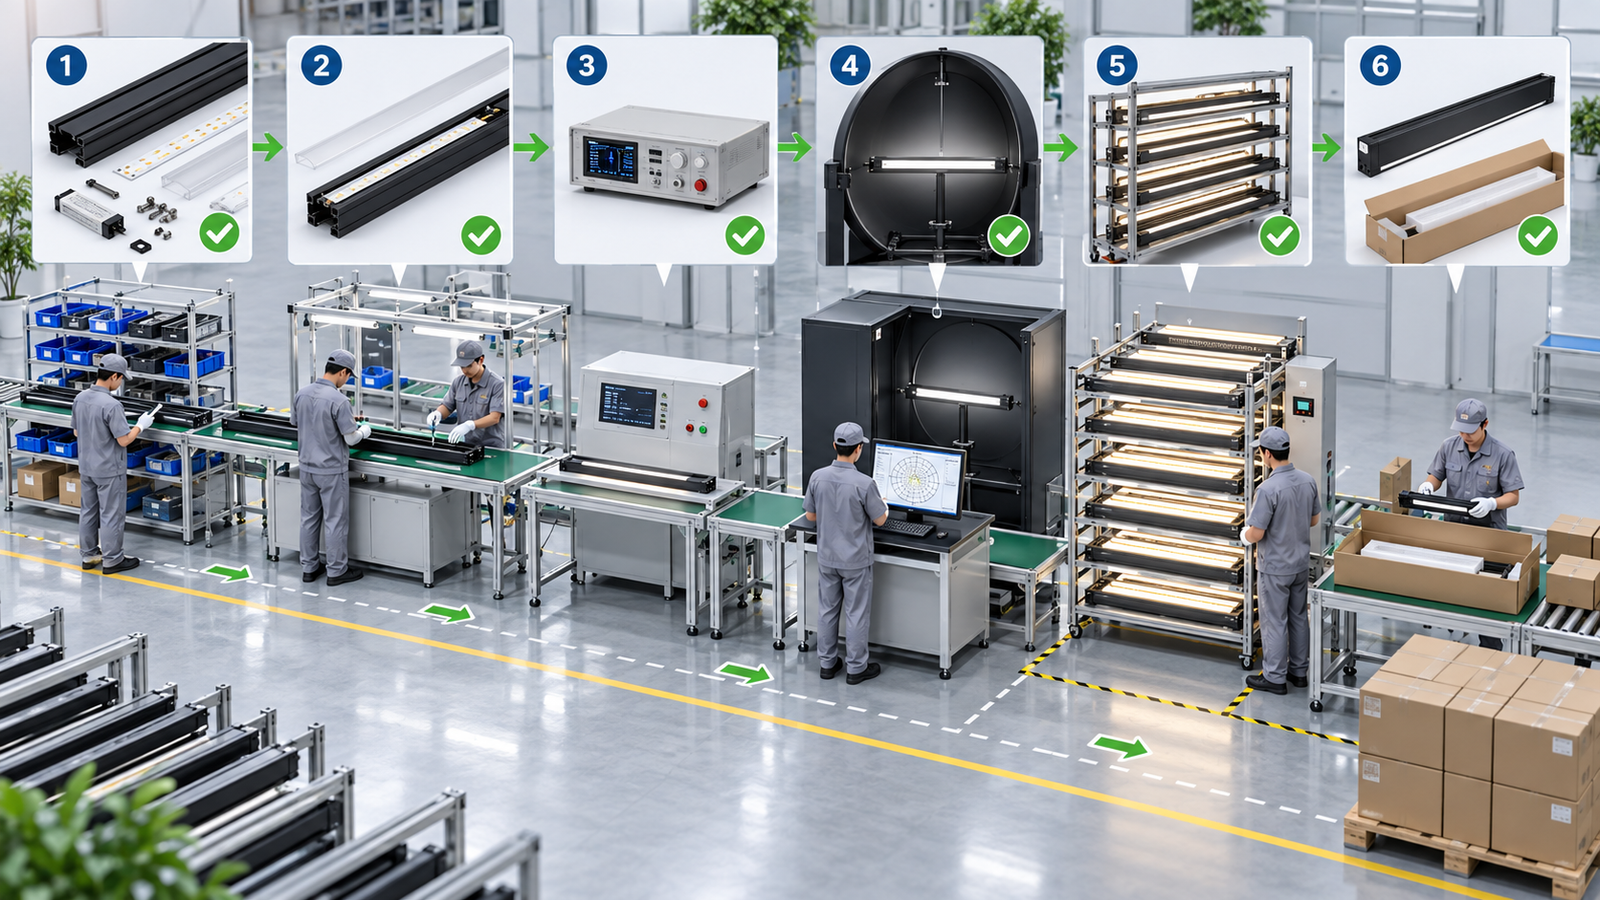
A factory tour can look impressive while the production order still changes driver, LED bin, optic or test method. OEM lighting quality is not proven by clean floors alone. It is created by a controlled chain from approved specification and incoming materials through assembly, testing, ageing, final inspection, packing and corrective action.
This checklist is for lighting brands, importers, distributors and project buyers evaluating LED track and linear light production. It helps you ask how the factory prevents defects, detects variation and traces problems. The goal is not to demand every test on every unit; it is to create controls proportional to the product and project risk.
Quality starts before the purchase order
Freeze what “good” means. Approve the model, power, lumens, optic, CCT, CRI, driver, control, adapter, finish, dimensions, weight, labels, instructions, packing and compliance-document set. Add tolerances and test methods. If the quotation says “or equivalent” for critical parts, define who approves the equivalent.
A quality team cannot protect a specification that remains vague. Use one configuration code on the purchase order, drawing, sample, production traveller and carton.
1. Supplier and factory qualification
Confirm the legal manufacturer, production address, product scope, capacity, key processes, subcontractors and quality responsibility. Review relevant management-system certificates where required, but also inspect how procedures are used on the floor. A certificate does not prove that your specific product is controlled.
Ask for examples of incoming inspection, first-article approval, nonconformance handling, calibration, training, traceability and change control. Review whether engineering and quality staff can explain recurring problems and corrective actions with data.
2. Contract and specification review
Before materials are purchased, the factory should review the order against drawings, bill of materials, compliance evidence and approved sample. Resolve conflicts between catalogue, quotation and purchase order. Confirm production quantity, spare parts, labels, language, test plan, inspection level and shipment date.
Create a risk list. New drivers, custom optics, unfamiliar adapters, high-power settings, tight colour tolerance and destination-specific labels deserve more attention than stable proven parts.
3. Bill of materials control
The bill of materials should identify manufacturer and part number for critical components: LEDs, driver, PCB, optics, cable, terminal, adapter, thermal material, fasteners and housing finish. Define approved alternatives and their evidence. Prevent purchasing from substituting a component solely because dimensions and price are similar.
Revision control matters. Production should use the released BOM, drawing and work instruction. Obsolete versions should be removed from workstations and electronic systems.
4. Incoming inspection
Incoming controls should match component risk. Verify identity, quantity, appearance, dimensions and supplier documentation. For LEDs, review manufacturer code, bin or colour data, packaging, moisture handling and traceability. For drivers, check model, ratings, label, connector and selected samples for function or electrical characteristics.
Optics should be checked for material, dimensions, surface defects and fit. Track adapters deserve dimensional, locking and contact verification against a controlled rail gauge or approved sample. Aluminium profiles and housings need dimensional and finish inspection.
5. Storage and material handling
Good incoming inspection is wasted if parts are mixed or damaged in storage. Use identified locations, lot separation, first-in/first-out rules where appropriate, electrostatic protection, moisture control and handling protection for optical surfaces. Quarantine nonconforming or unapproved materials physically and electronically.
Keep traceability when materials are split into work orders. A batch code should lead back to the component lot without requiring staff memory.
6. First-article inspection
Before full production, build the first unit or small set using production tooling and operators. Compare it with the approved drawing and golden sample. Check dimensions, assembly, wiring, fasteners, thermal interfaces, adapter, optics, panel movement, labels and function.
Measure power, luminous output, colour and beam characteristics appropriate to the control plan. Review the first article with engineering and quality, record deviations and authorise production formally.
7. Assembly process control
Work instructions should show component orientation, cable routing, connection, insulation, earthing, thermal-material placement, screw sequence and torque where critical. Use fixtures or error-proofing to prevent reversed parts and mixed optics. Operators should know what defects require stopping the line.
For adjustable track luminaires, control hinge or friction mechanisms so panels hold position without being excessively stiff. Verify that cables are not pinched through the full movement range.
8. In-process electrical checks
Electrical safety and function tests should follow the applicable product requirements and approved control plan. Depending on construction, this may include protective continuity, dielectric or insulation-related tests, polarity, functional operation and visual inspection. Test equipment and limits must be defined by qualified personnel.
Record results by batch or unit according to risk. Failed units should be segregated; simply retesting until a pass without finding the cause hides process problems.
9. Power and driver verification
Measure representative units at stated voltage and frequency after suitable stabilisation. Review input power, current, power factor and any other specified characteristics. Test selectable wattage positions and dimming or control modes. Confirm the driver model against the BOM.
If a parameter trends toward a limit, investigate before the shipment fails. Control charts or simple trend graphs can reveal drift even when individual units still pass.
10. Photometric and colour control
Use calibrated equipment appropriate to the measurement. An integrating sphere can support flux, efficacy, CCT, CRI and chromaticity checks; a goniophotometer supports intensity distribution and photometric files. Production may use faster correlated methods after the relationship to laboratory equipment is established.
Define sample size, stabilisation, ambient, measurement tolerance and acceptance limits. Compare both panels of a dual-panel light and multiple units within the batch. Monitor colour consistency, not only average CCT.
11. Beam and optic verification
Wrong optics are easy to install and difficult to notice on a bright factory floor. Verify optic code and orientation. Use a controlled screen, intensity measurement or photometric sampling to compare beam shape, angle, symmetry and artefacts with the approved reference.
For 60° and 90° versions, keep parts physically separated and label work-in-process. Do not identify them only by operator memory.
12. Flicker and dimming checks
If temporal-light performance is specified, use a defined instrument and metric. Test full output and relevant dimmed levels with the production driver. For phase-cut products, the approved dimmer and representative load should be used. For 0–10V or DALI, check response, minimum level and recovery.
A phone camera can help spot obvious anomalies but should not replace PstLM, SVM or other required measurements.
13. Thermal verification
Confirm assembly features that control heat: LED board contact, thermal pad or compound coverage, driver placement and ventilation. Periodically verify temperatures or thermal performance on production-intent units under the defined worst relevant condition.
A thermal design validated on a sample can be undermined by a missing pad, loose fastener or substituted driver. Make critical thermal steps visible in inspection records.
14. Mechanical and adapter checks
Measure dimensions, straightness, fit, rotation, tilt, holding force and fastener security. Test the track adapter with a controlled reference rail for insertion, selection, locking and retention. For long fixtures, inspect balance and leverage at intended orientations.
Cycle adjustable parts enough to screen assembly problems without presenting a short cycle as a lifetime test. Define separate reliability testing where needed.
15. Appearance and finish inspection
Agree viewing distance, lighting, defect categories and acceptance samples for scratches, colour variation, coating texture, gaps, exposed fasteners, lens marks and contamination. Black finishes reveal dust and handling marks; optical surfaces should be protected until final cleaning.
Use boundary samples showing acceptable and unacceptable conditions. Written phrases such as “no obvious defect” are interpreted differently by each inspector.
16. Ageing or burn-in
An ageing process can screen early failures, poor connections and unstable components. Define duration, input condition, switching, ambient, rack loading and pass criteria. Record failures by cause. Longer is not automatically better if conditions are uncontrolled.
Burn-in does not prove a 50,000-hour lifetime. Long-term lumen maintenance and component reliability require different evidence. Use ageing as one production screen within a broader reliability plan.
17. Final inspection
Before packing, confirm model, configuration, function, appearance, movement, adapter, accessories, labels and instructions. Verify that corrective work has been re-inspected. Use a documented sampling plan appropriate to order value and risk, with critical, major and minor defect categories.
For first orders or custom models, add a shipment hold point until the buyer or authorised inspector approves the final report.
18. Packaging validation
Packaging must protect the fixture, moving panels, optics, adapter and finish through real distribution. Review inner supports, abrasion protection, carton strength, accessory containment and orientation. Conduct agreed drop, vibration or transport simulation where the project requires it.
Check carton labels, model suffix, quantity, destination marks and pallet plan. Mixed wattages or optics should be easy to identify at receiving.
19. Nonconformance and corrective action
When a unit fails, record defect, lot, station, disposition and cause. Separate rework, repair, scrap and use-as-is decisions. Significant deviations need authorised review, and the buyer should approve changes affecting agreed requirements.
Corrective action should identify root cause, containment, permanent action and verification of effectiveness. Replacing the failed unit without improving the process allows recurrence.
20. Change control
Require advance notice for changes to LEDs, drivers, PCBs, optics, adapters, thermal materials, suppliers, factory location, process, tooling, firmware, labels or compliance documents. Classify changes by risk and define whether engineering review, testing or a new sample is needed.
Maintain a revision history linked to production dates and batch codes. This protects repeat-order consistency and field investigations.
21. Traceability
A batch or serial code should connect finished product to work order, BOM revision, critical component lots, production date, test records and inspection result. The granularity should reflect risk and service needs. Test the traceability system during the audit by selecting a random unit and tracing backward and forward.
22. Calibration and measurement confidence
List measuring equipment, calibration status, verification intervals and reference standards. Protect instruments from damage and environmental influence. When a device is found out of calibration, assess product measured since the last valid check.
Measurement uncertainty should be considered near acceptance limits. A reported 100.0 is not exact merely because the display has decimals.
23. Training and workmanship
Operators and inspectors need training for their tasks, defects and stop rules. Verify competence through observation and records, not attendance signatures alone. Temporary staff and new models deserve additional supervision.
24. Pre-shipment report
Request a concise package containing order configuration, quantity, batch codes, inspection sampling, defects and disposition, electrical and functional results, photometric and colour samples, ageing record, label and packing photographs, and document revision list. The report should be reviewed before release.
Factory audit questions
- How is the approved sample linked to the BOM and work order?
- Which components cannot change without buyer approval?
- How are LED bins, drivers and optics prevented from mixing?
- What tests are performed on every unit and by sampling?
- How are instruments calibrated and verified?
- What happens immediately when a unit fails?
- Can a finished unit be traced to component lots?
- How are reworked products identified and reinspected?
- How are customer complaints converted into process action?
- Can the factory show evidence that corrective actions remained effective?
Build a control plan
Create a table with process step, characteristic, specification, method, equipment, frequency, sample size, responsible person, record and reaction plan. Review it during sample approval and before every major change. The control plan turns expectations into repeatable work.
Our RFQ and sample-approval guide helps establish the configuration that the control plan must protect.
Final recommendation
A strong OEM factory does not promise zero defects. It shows how risks are controlled, how variation is measured, how failures are contained and how production remains consistent with the approved sample. Evaluate the system behind the product, not only the showroom sample.
If you send us your product specification, destination and quality requirements, we can prepare a model-specific control plan and pre-shipment record. We prefer measurable acceptance criteria because they protect the buyer, factory and final project at the same time.
